
PA-CF print settings
Carbon Fibre Reinforced Nylon · Advanced
PA-CF (Carbon Fibre Reinforced Nylon) prints at 260-280°C with the bed at 80-100°C. It needs an enclosure. Dry the filament before printing.
Nylon with chopped carbon fibre. Much stiffer and more dimensionally stable than plain nylon, and abrasive enough to destroy a brass nozzle in a single print.
Settings at a glance
Ranges are typical manufacturer-published figures for this material class, not measurements we took. Always start with your filament maker’s own numbers where they differ. The price is an indicative street price for a 1 kg spool, not a live quote.
Good for
- Structural brackets
- Drone frames
- Jigs and fixtures
- Parts that must not flex
Avoid for
- Brass nozzles
- Parts needing a smooth cosmetic finish
- Transparent parts
The problem people actually hit
Underextrusion that gets worse as the print goes on. The carbon fibre has widened the nozzle bore. Fit a hardened steel or ruby nozzle before the first print, not after.
Drying
Hygroscopic. Dry at 70-80C for 8-12 hours.
If your printer cannot run PA-CF
PA-CF needs an enclosure, a dry box and a hot end comfortable at 260-280°C. That is a real hardware investment for a single part. If you need one bracket rather than a new capability, buying the machine time is usually the cheaper answer.
A print service already owns the machine. You upload the model, choose PA-CF, and a part arrives. For a one-off this is almost always cheaper than the equipment, and it is the only route if your printer tops out below 260°C.
Industrial supplier with the widest confirmed engineering-material range, including certified work.
Low-cost industrial capacity. Usually the cheapest route for a one-off part.
Confirm the service actually offers PA-CF before uploading. Material menus change, and a service that lists dozens of options may not carry this one. We have no commercial relationship with any of these companies, and these are ordinary links.
Buying PA-CF
PA-CF is stocked unevenly by general retailers. A specialist supplier is usually the better source, both for availability and because they publish the spec sheet. Typical street price is $60-120 per 1 kg spool.
Check before you order
- Diameter 1.75mm unless your printer takes 2.85mm. Check before ordering, not after.
- Published diameter tolerance. ±0.02mm is good, ±0.05mm is loose and shows up as inconsistent extrusion.
- Vacuum-sealed with desiccant. Hygroscopic filament that shipped open has already absorbed moisture and will need drying before its first print.
- Fit a hardened nozzle first. This material is abrasive and will widen a brass nozzle within a print or two.
- Confirm you have an enclosure before buying. Without one this material will warp regardless of spool quality.
Specialist suppliers
Deep engineering-material catalogue and published spec sheets, including grades general retailers do not stock.
Specialist stockist with strong coverage of nylon and carbon-fibre filled materials.
Named because they stock this class of material and publish specifications. We have no commercial relationship with either, and these are ordinary links.
Amazon listings for PA-CF are often mislabelled or relabelled stock. Verify the datasheet before ordering.
Not sure this is the right material? Compare all materials.
Need the finished part instead of another spool of PA-CF?
Upload the model and get a price. PA-CF is one of the materials the service prints.
PA-CF is quoted by a person rather than instantly, so expect a reply rather than a price on the spot.
FDM only, up to 220mm per side, shipping within the United States. Accepts STL, 3MF, STEP, OBJ.
Get a quoteOwnership: 3DPrinterOnDemand is Another Anvil Road property, so we have a commercial interest in it. We are not recommending it as an independent party, and where it cannot print a material we say so and point elsewhere.
What you need to print PA-CF
Gear that PA-CF genuinely requires, with the specification that decides whether a given unit will actually work.
Filament dryer
Must reach at least 70C
PA-CF will not print cleanly wet, and many budget dryers stop at 55-60C. Check the maximum temperature before buying, not the marketing copy.
See filament dryer on AmazonPrinter enclosure
Fully closed, with a door
PA-CF warps when a draught cools the part unevenly. An enclosure holds chamber heat steady, which fixes lifting corners and split layers more reliably than any slicer setting.
See printer enclosure on AmazonBed adhesion
PEI sheet sized to your bed, or a PVP glue stick
PA-CF lifts at the corners before it fails anywhere else. A textured PEI surface plus a thin glue layer holds the first layer down while the chamber comes up to temperature.
See bed adhesion on AmazonHeat-set threaded inserts
Brass, M3 unless your design says otherwise
Printed threads strip. If you are making structural brackets out of PA-CF, melting brass inserts in gives you a metal thread that survives being undone more than once.
See heat-set threaded inserts on AmazonHardened steel nozzle
Hardened steel or ruby, matching your hot end
PA-CF is abrasive and will widen a brass nozzle within a print or two. Fit the hardened nozzle before the first print - the symptom, worsening underextrusion, looks like a dozen other faults.
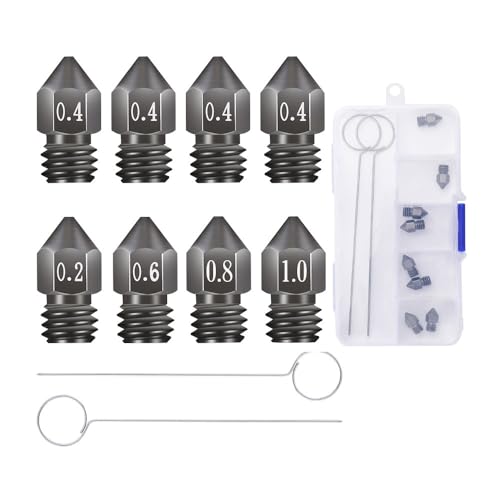 Creality · Hardened steel nozzles, MK8Hardened steel for abrasive filament. MK8 is a thread pattern, not a universal fit
Airtight storage with desiccant
Sealed container plus rechargeable desiccant
Drying a spool once achieves nothing if it sits open afterwards. Storage is what keeps the filament usable between prints.
See airtight storage with desiccant on AmazonAs an Amazon Associate we earn from qualifying purchases. Links above are affiliate links, and using them costs you nothing extra.
PA-CF questions
- What temperature do you print PA-CF at?
- PA-CF prints at a nozzle temperature of 260-280C with the bed at 80-100C. Start at the lower end of the nozzle range and raise it in 5C steps until layers bond cleanly.
- Does PA-CF need an enclosure?
- Yes. PA-CF needs an enclosure. Without one the part cools unevenly, corners lift off the bed and layers split partway up the print.
- Do you need to dry PA-CF?
- Hygroscopic. Dry at 70-80C for 8-12 hours.
- What is PA-CF good for?
- PA-CF suits structural brackets, drone frames, jigs and fixtures, parts that must not flex. Avoid it for brass nozzles, parts needing a smooth cosmetic finish, transparent parts.
- How much does PA-CF cost?
- A 1 kg spool of PA-CF typically sells for $60-120. That is an indicative street price rather than a live figure, so check the retailer for today's cost.
PA-CF or PC?
PC (Polycarbonate) prints at 260-310°C with a 100-120°C bed and needs an enclosure. The strongest and most heat resistant material most desktop printers can run. Genuinely tough, genuinely difficult, and it demands a hot end that can hold 300C.
Read the PC settings guide →After the print
The workshop steps that matter most for PA-CF.